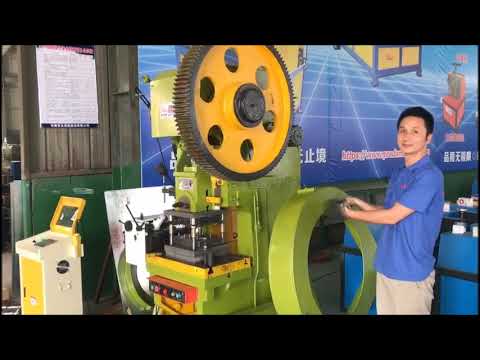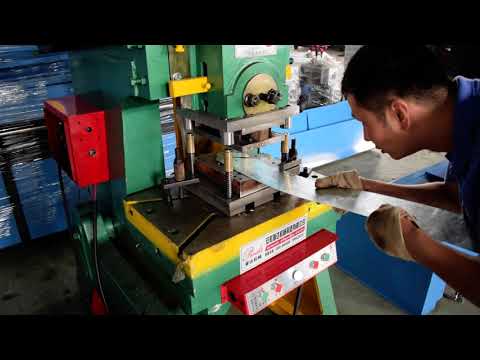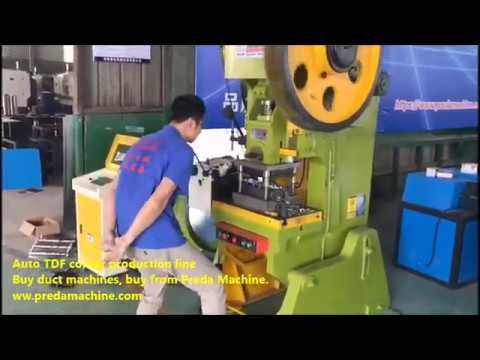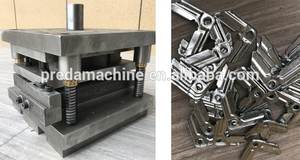


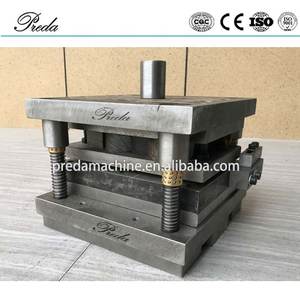
TDF Corner Mold PD-01
Last updated: October 12, 2026
Precision TDF corner mold for producing standard TDF flange corners from galvanized or stainless steel sheet.
Technical Specifications
What is a TDF Corner Mold PD-01?
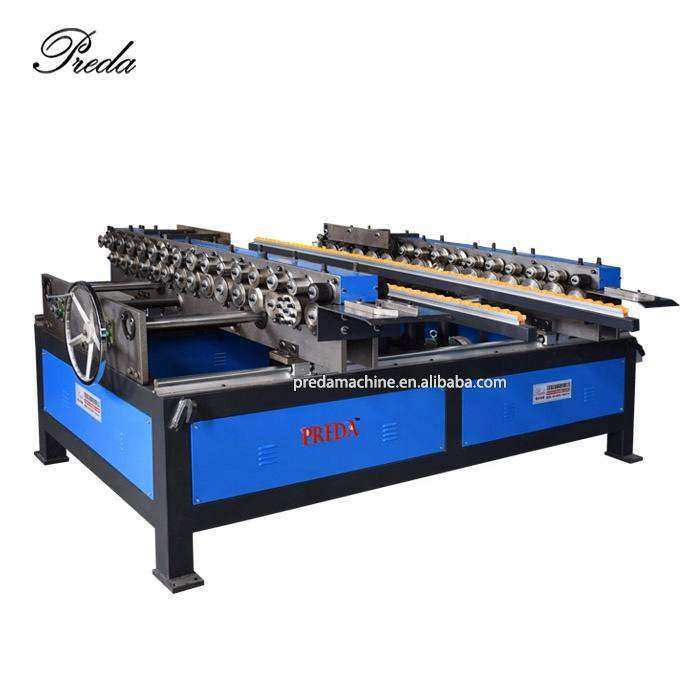
A flange forming machine is sheet metal equipment that produces TDF (Transverse Duct Flange) or TDC (Transverse Duct Connector) flanges on the edges of rectangular duct panels. These flanges allow duct sections to be bolted together with gaskets for air-tight connections. Flange formers are typically used in conjunction with auto duct lines or as standalone machines for custom ductwork fabrication.
Key Features
- Precision-ground tool steel
- Consistent 90-degree corners
- Compatible with standard punch presses
- Quick installation
- Long service life
Still Losing Money to Slow Flange Installation and Poor Seals?
Every HVAC duct shop faces the same bottleneck: manual flange forming and riveting. When your team spends hours on inconsistent flange dimensions, your production capacity drops, labor costs rise, and deadlines slip. The TDF Corner Mold PD-01 is engineered to eliminate these inefficiencies — automating TDF corner mold while delivering consistent, factory-grade quality.
In this guide, we break down exactly how this machine transforms your PD-01 corner die workflow, what specifications matter for your operation, and how to calculate your return on investment. Whether you run a 3-person job shop or a 50-employee production facility, understanding these details directly impacts your bottom line.
How It Transforms Your Production Line
The TDF Corner Mold PD-01 operates on a proven principle: TDF corner mold should be a continuous, automated process — not a series of manual interventions. Here is the step-by-step workflow that makes this possible:
Panel Feeding
The duct panel edge is fed into the flange forming rollers, with adjustable guides ensuring proper alignment.
Flange Roll Forming
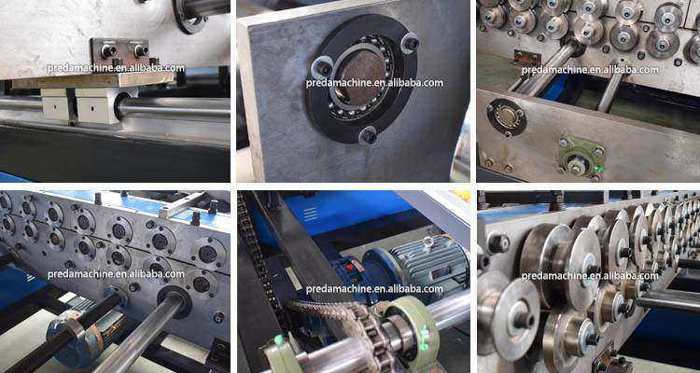
Multiple roller stations progressively form the TDF/TDC flange profile — creating the integral flange that replaces traditional angle iron frames.
Corner Notching (Optional)
Integrated notching stations cut the corner reliefs needed for clean 90° flange corners.
Corner Crimping
Hydraulic or pneumatic corner tools crimp the flange corners, creating a rigid, square connection point.
Technical Specifications & Performance Data
Every specification on this machine is chosen for a reason. The table below shows not just the numbers, but what each one means for your daily production:
| Parameter | This Machine | What It Means for You |
|---|---|---|
| Control System | PLC with touchscreen | Easy programming, consistent results, minimal training |
| Construction | Heavy-duty steel frame | Vibration-free operation, 10+ year service life |
| Certification | CE certified | Meets European safety and quality standards |
| Warranty | 2 years | Peace of mind with comprehensive factory warranty |
Problems Solved: Before vs. After
We asked 50+ HVAC fabricators about their biggest production headaches. Here is how this machine directly addresses each one:
| Without This Machine | With This Machine |
|---|---|
|
✕ Angle iron flanges are heavy and slow
Welding angle iron takes 10-15 min per duct, adds weight |
✓ TDF integral flange formed in seconds
Flange time reduced to 30 seconds, 40% lighter |
|
✕ Flanges don't align on site
Gaps between flanges cause air leakage, need shimming |
✓ CNC-formed flanges with ±0.3mm accuracy
Perfect flange alignment, gasket seals every time |
|
✕ Riveting is slow and labor-intensive
Each flange needs 8-12 rivets, 5-10 minutes per duct |
✓ TDF flange is integral — no rivets needed
Eliminate riveting entirely, save 70% assembly time |
|
✕ Corner gaps and leaks
Poor corner construction is the #1 leak source |
✓ Hydraulic corner crimping creates tight corners
Leakage class C compliance, no corner leaks |
Where It Fits in Your Factory
This machine is versatile enough to serve multiple production scenarios. Here are the most common configurations our customers use:
Commercial HVAC Ductwork
TDF flanges are the global standard for commercial rectangular duct connections — used in offices, hospitals, schools, and retail.
Industrial Ventilation
TDC flanges for high-pressure industrial systems where heavier gauge and stronger connections are required.
Duct Retrofit & Replacement
Upgrading old angle-iron duct systems to modern TDF flange technology for better sealing and faster installation.
Prefabrication Facilities
High-volume duct prefab shops where consistent flange quality is essential for just-in-time delivery to construction sites.
Frequently Asked Questions
Click each question to see the answer. These are the questions our sales engineers hear most often:
TDF Corner Mold PD-01: Which Die You Actually Need
A corner mold is a wear item, not a machine, and buying the wrong one is the most common small purchase mistake in a duct shop. The PD-01 is the standard TDF corner die. Confirm three things before ordering: flange height, gauge range, and the press or machine it will be fitted to.
| Item | Purpose | Fits | Note |
|---|---|---|---|
TDF Corner Mold PD-01 This item — standard TDF corner die | Forms and crimps the TDF corner insert Consumable tooling | TDF corner making machines and standard presses Check the shank before ordering | The spare to keep on the shelf Wears faster than any other tooling in the shop |
The TDC equivalent | Corner insert for the TDC profile Different profile | TDC corner stations Not interchangeable with PD-01 | Only for TDC work TDF and TDC corners look similar and are not interchangeable |
Clamp-mounted TDC die | Portable TDC corner work Clamps to a bench | Bench or site use Low volume | Site work or occasional TDC corners Slower than a fixed station but needs no machine |
The machine this die fits | Dedicated corner station Operator-paced | Accepts the PD-01 The standard pairing | If you are buying the machine, order a spare die with it Downtime waiting for a die costs more than the die |
Alternative for heavier gauge | Hydraulic crimping without a fixed press Higher force | Its own tooling Portable | Heavier gauge or crimping at the assembly point Different tooling from the PD-01 |
Getting the Life You Paid For Out of a Corner Die
Corner dies fail from wear, contamination and misalignment — rarely from defects. These steps typically double die life in a busy shop.
- 1. The die is cut for a specific flange height. A die for a 30 mm flange on a 35 mm flange produces a corner that neither fits nor holds.
- 2. The PD-01 fits standard TDF corner machines, but presses vary. Measure the shank before assuming a fit.
- 3. Height first, depth second. Setting depth first is the usual cause of corners that fit but do not hold.
- 4. Zinc build-up in the die cavity changes the crimp geometry gradually, so quality drifts rather than failing suddenly. A brass brush at shift end prevents it.
- 5. Lubricant on the forming faces attracts zinc dust and accelerates wear.
- 6. Look for rounding on the crimp edges. Once the edge is round, the corner stops holding even though the die looks serviceable.
- 7. Hang it at the station. Operators can compare a suspect corner in seconds instead of guessing.
- 8. Lead time on tooling is longer than the remaining life of a die showing wear. Buy the spare while the first is still good.
Corner Die Faults: Symptom, Cause, Fix
Die problems announce themselves as corner quality that slowly drifts. Catching the drift early is the whole game.
| Symptom | Most likely cause | What to do |
|---|---|---|
Corner quality slowly declines over weeks Wear on the crimp edges | Gradual rounding of the die edge, so the crimp gets shallower over time Drift rather than sudden failure is the signature of wear | Inspect the die edge under a bright light and compare with a new one Replace when the edge shows rounding — do not compensate with depth |
Zinc build-up in the die cavity No cleaning routine | Galvanising transfers to the die and accumulates Changes geometry slowly, so it is often missed | Clean with a brass brush at the end of every shift Never use steel — it damages the die surface |
Corner will not seat at all Wrong die for the flange height | The profile does not match, so no amount of force will seat it Forcing it damages both the die and the flange | Confirm flange height and die specification before applying force Mark every die with the flange height it is cut for |
Die cracked or chipped Misalignment, or material over specification | A die that is mounted out of square takes load on one edge Or material thicker than the die was specified for | Check mounting alignment and measure the material thickness A cracked die is finished — replace it, do not weld it |
Crimp depth inconsistent across the batch Press or machine wear, not the die | Lost motion in the press ram shows as depth variation Blaming the die is the common mistake | Check the ram for play before replacing the die Measure depth on five consecutive corners |
Corner holds but looks wrong Die correct, cosmetic issue only | A corner can be structurally sound and visually poor, usually from coating damage Worth checking because coating damage leads to corrosion | Check for galvanising cracking; if absent and the pull test passes, accept it Do not adjust a working set-up for appearance alone |
Professional Packaging & Global Shipping
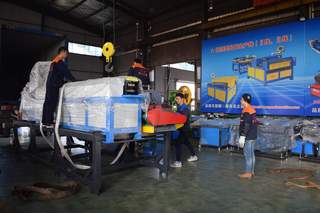
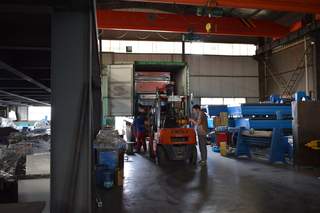
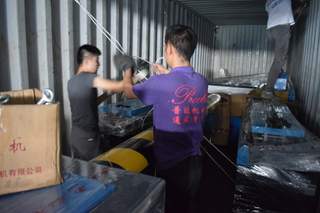
Every machine is professionally packaged and secured in a container for safe delivery to your port. We send you loading photos before the ship sails.
Calculate Your Return on Investment
Based on average industry data, here is what a typical customer saves after installing this machine:
* Figures based on average customer data for a shop producing 300-800 duct sections per month. Your actual results will vary based on production volume, labor rates, and current efficiency levels. Contact our engineers for a customized ROI calculation based on your specific operation.
Ready to Upgrade Your TDF Production?
Get a customized quote within 24 hours. Our engineers will help you configure the right machine for your specific production requirements.
WhatsApp / WeChat: +86-18355321923 | Email: jason@predamachine.com
Related Products

Buying Guides for This Machine Type
Before you request a quote: how this machine class compares, what it costs, and how to size it for your production volume.
TDF Corner Making Guide 2026
Corner machine vs corner matics vs hand molds: the real cost per corner at different volumes.
Read the guide → ComparisonTDF vs TDC Flange Guide
The two dominant rectangular duct flange systems compared on sealing, speed and installed cost.
Read the guide → Buying GuideTDF Flange Former Buying Guide 2026
T-12 vs T-16 vs Duplex vs Dual Head — throughput, gauge range and shop-size fit.
Read the guide → ComparisonTDF Bender: Electric vs Pneumatic
Power source choice for TDF benders — air supply requirements, cycle speed and maintenance load.
Read the guide →