

G Clamp Mold for TDC Flange PD-03
Last updated: October 12, 2026
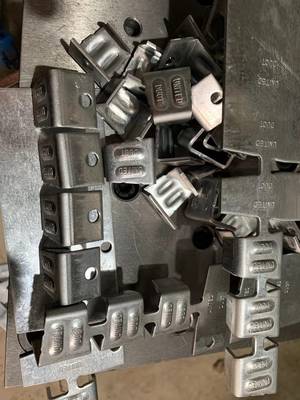
G-clamp mold for TDC flange fastening, essential tool for secure and efficient TDC duct connection assembly.
Technical Specifications
What is a G Clamp Mold for TDC Flange PD-03?
A flange forming machine is sheet metal equipment that produces TDF (Transverse Duct Flange) or TDC (Transverse Duct Connector) flanges on the edges of rectangular duct panels. These flanges allow duct sections to be bolted together with gaskets for air-tight connections. Flange formers are typically used in conjunction with auto duct lines or as standalone machines for custom ductwork fabrication.
Key Features
- Produces G-clips for TDC system
- Secure flange fastening solution
- Hardened tool steel for durability
- Precision forming
- Compatible with standard punch presses
Still Losing Money to Slow Flange Installation and Poor Seals?
Every HVAC duct shop faces the same bottleneck: manual flange forming and riveting. When your team spends hours on inconsistent flange dimensions, your production capacity drops, labor costs rise, and deadlines slip. The G Clamp Mold for TDC Flange PD-03 is engineered to eliminate these inefficiencies — automating G clamp mold TDC while delivering consistent, factory-grade quality.
In this guide, we break down exactly how this machine transforms your PD-03 G-clip workflow, what specifications matter for your operation, and how to calculate your return on investment. Whether you run a 3-person job shop or a 50-employee production facility, understanding these details directly impacts your bottom line.
How It Transforms Your Production Line
The G Clamp Mold for TDC Flange PD-03 operates on a proven principle: G clamp mold TDC should be a continuous, automated process — not a series of manual interventions. Here is the step-by-step workflow that makes this possible:
Panel Feeding
The duct panel edge is fed into the flange forming rollers, with adjustable guides ensuring proper alignment.
Flange Roll Forming
Multiple roller stations progressively form the TDF/TDC flange profile — creating the integral flange that replaces traditional angle iron frames.
Corner Notching (Optional)
Integrated notching stations cut the corner reliefs needed for clean 90° flange corners.
Corner Crimping
Hydraulic or pneumatic corner tools crimp the flange corners, creating a rigid, square connection point.
Technical Specifications & Performance Data
Every specification on this machine is chosen for a reason. The table below shows not just the numbers, but what each one means for your daily production:
| Parameter | This Machine | What It Means for You |
|---|---|---|
| Control System | PLC with touchscreen | Easy programming, consistent results, minimal training |
| Construction | Heavy-duty steel frame | Vibration-free operation, 10+ year service life |
| Certification | CE certified | Meets European safety and quality standards |
| Warranty | 2 years | Peace of mind with comprehensive factory warranty |
Problems Solved: Before vs. After
We asked 50+ HVAC fabricators about their biggest production headaches. Here is how this machine directly addresses each one:
| Without This Machine | With This Machine |
|---|---|
|
✕ Angle iron flanges are heavy and slow
Welding angle iron takes 10-15 min per duct, adds weight |
✓ TDF integral flange formed in seconds
Flange time reduced to 30 seconds, 40% lighter |
|
✕ Flanges don't align on site
Gaps between flanges cause air leakage, need shimming |
✓ CNC-formed flanges with ±0.3mm accuracy
Perfect flange alignment, gasket seals every time |
|
✕ Riveting is slow and labor-intensive
Each flange needs 8-12 rivets, 5-10 minutes per duct |
✓ TDF flange is integral — no rivets needed
Eliminate riveting entirely, save 70% assembly time |
|
✕ Corner gaps and leaks
Poor corner construction is the #1 leak source |
✓ Hydraulic corner crimping creates tight corners
Leakage class C compliance, no corner leaks |
Where It Fits in Your Factory
This machine is versatile enough to serve multiple production scenarios. Here are the most common configurations our customers use:
Commercial HVAC Ductwork
TDF flanges are the global standard for commercial rectangular duct connections — used in offices, hospitals, schools, and retail.
Industrial Ventilation
TDC flanges for high-pressure industrial systems where heavier gauge and stronger connections are required.
Duct Retrofit & Replacement
Upgrading old angle-iron duct systems to modern TDF flange technology for better sealing and faster installation.
Prefabrication Facilities
High-volume duct prefab shops where consistent flange quality is essential for just-in-time delivery to construction sites.
Frequently Asked Questions
Click each question to see the answer. These are the questions our sales engineers hear most often:
G Clamp Mold TDC PD-03: A Bench Tool, Not a Production Station
The PD-03 is a clamp-mounted TDC corner die. It exists for the jobs a fixed corner station cannot reach: site work, one-off ducts, and shops that make TDC corners occasionally rather than all day. If you are making more than about 100 corners a day, a fixed station will pay for itself in labour within a few months.
| Option | Corners per hour | Needs | Choose it when |
|---|---|---|---|
G Clamp Mold TDC PD-03 This item — clamp-mounted TDC die | 40–80 Operator-paced and manually clamped | A bench and a hammer or press No machine, no air, no power | Site work, one-off ducts, or occasional TDC corners Also the sensible backup die for a shop that normally uses a station |
The fixed-station TDC die | 300–600 Machine-paced | A corner making machine or press Fixed installation | TDC corners are routine rather than occasional The PD-03 will become the bottleneck above ~100 corners a day |
The TDF equivalent | Depends on the machine Different profile | TDF corner station Not interchangeable | Your work is TDF rather than TDC TDF and TDC corners look similar and do not interchange |
Forms the TDC flange itself | Not comparable Different operation | Power and floor space The upstream machine | You need to form TDC flange, not just corners The PD-03 only finishes what the former started |
Hydraulic portable crimping | 300–500 Higher force per stroke | Hydraulic unit Heavier gauge work | You need portability and more force than a clamp die gives Different tooling from the PD-03 |
Getting Clean TDC Corners From a Clamp Die
A clamp-mounted die is only as consistent as the surface it is clamped to and the discipline of the operator. These steps remove most of the variation people blame on the die.
- 1. A die that moves under the stroke produces a corner that is partly formed. Clamp to something that does not flex, and check the clamp before every batch.
- 2. TDC connectors vary between suppliers by a millimetre or two. A die cut for one pattern will produce corners that look right and do not engage with another.
- 3. Most bad clamp-die corners are corners that were not seated. Make seating a deliberate step rather than something that happens on the way to the stroke.
- 4. Over-striking fractures the galvanising at the corner, which is where duct corrosion starts. Find the minimum stroke that fully forms the corner and stay there.
- 5. Zinc build-up changes the crimp geometry slowly, so quality drifts rather than failing suddenly. A brass brush takes ten seconds.
- 6. Pull a corner apart and look at the failure. If the metal tears rather than the joint opening, the joint is stronger than the material and the corner is correct.
- 7. Operators can compare a suspect corner in seconds instead of arguing about whether it looks acceptable.
- 8. If you are clamping and unclamping more than about 100 times a day, the labour cost has already exceeded a fixed station. Move up rather than working around it.
Clamp Die Faults: Symptom, Cause, Fix
Almost every clamp-die problem is seating, force or the wrong die pattern. All three are quick to check without tools.
| Symptom | Most likely cause | What to do |
|---|---|---|
Corner partly formed Die moved during the stroke, or flange not seated | The clamp was not tight, or the bench flexed By far the most common fault with a clamp-mounted die | Re-clamp to a solid surface and make seating a deliberate step Check the clamp before each batch, not once a day |
Galvanising cracks at the corner Excessive stroke force | Over-forming fractures the coating, and that is where corrosion begins Looks like a strong corner but fails early in service | Find the minimum stroke that fully forms the corner and standardise on it A consistent moderate stroke beats a hard one |
Corner will not accept the connector Die pattern does not match the connector | TDC connectors vary between suppliers Forcing it damages both the die and the flange | Confirm the connector part number against the die specification before applying force Keep the connector sample with the die |
Corner quality varies between operators No standardised seating and stroke | With a hand tool, the operator is the process Variation is normal until the steps are written down | Write the three steps on a card fixed at the bench and train against it Record a short video — it is faster than retraining verbally |
Zinc accumulating in the die cavity No cleaning routine | Galvanising transfers and builds up, changing geometry gradually Easy to miss because the change is slow | Clean with a brass brush after each use — never steel, which damages the die Inspect under a bright light weekly |
Die cracked Struck off-axis or material over specification | A clamp die takes load unevenly if the stroke is not square Or the material is thicker than the die was cut for | Replace the die — a cracked die is finished, not repairable Check material thickness before fitting the replacement |
Professional Packaging & Global Shipping
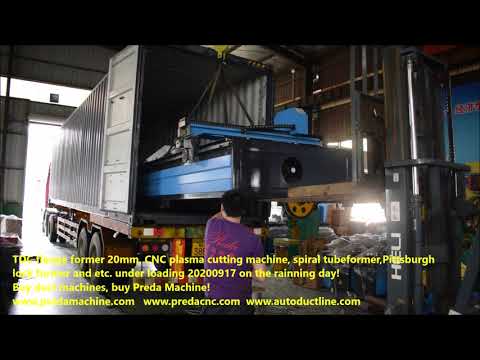
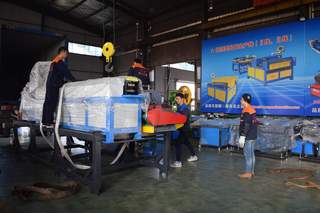
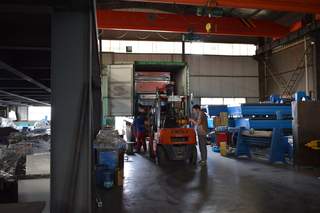
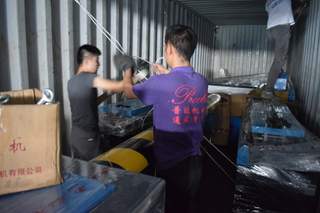
Every machine is professionally packaged and secured in a container for safe delivery to your port. We send you loading photos before the ship sails.
Calculate Your Return on Investment
Based on average industry data, here is what a typical customer saves after installing this machine:
* Figures based on average customer data for a shop producing 300-800 duct sections per month. Your actual results will vary based on production volume, labor rates, and current efficiency levels. Contact our engineers for a customized ROI calculation based on your specific operation.
Ready to Upgrade Your G Production?
Get a customized quote within 24 hours. Our engineers will help you configure the right machine for your specific production requirements.
WhatsApp / WeChat: +86-18355321923 | Email: jason@predamachine.com
Related Products

Buying Guides for This Machine Type
Before you request a quote: how this machine class compares, what it costs, and how to size it for your production volume.
TDF vs TDC Flange Guide
The two dominant rectangular duct flange systems compared on sealing, speed and installed cost.
Read the guide → Buying GuideTDF Corner Making Guide 2026
Corner machine vs corner matics vs hand molds: the real cost per corner at different volumes.
Read the guide → Buying GuideTDF Flange Former Buying Guide 2026
T-12 vs T-16 vs Duplex vs Dual Head — throughput, gauge range and shop-size fit.
Read the guide → ComparisonTDF Bender: Electric vs Pneumatic
Power source choice for TDF benders — air supply requirements, cycle speed and maintenance load.
Read the guide →