Quality in duct fabrication is not discovered at the pressure test - it is decided at the blank cutter, the lockformer, the seam closer and the flanging bench. A defect caught at the blank stage costs minutes to fix; the same defect found after assembly costs a section, a rework cycle and a missed deadline. This guide maps the quality control checkpoints from coil to installed section, lists the defects that actually show up in shops, and shows which machine decisions prevent them before they exist.
The Cost of Catching Defects Late
Rework arithmetic is brutal and predictable. A notch cut wrong on a blank is corrected with a few minutes of re-cutting. A seam closed unevenly is a section that fails the pressure test - and the rework happens after the section is assembled, sealed and possibly moved to the site. The industry rule of thumb holds in every shop: the cost of a defect multiplies by roughly ten for each stage it survives. That is why quality control is placed at the process, not at the end of it, and why the machines that hold geometry repeatably are quality equipment first and speed equipment second.
Quality Checkpoints Across the Workflow
The table below is the QC map for a rectangular duct shop, and it applies whether the blank comes from a manual shear or a full auto duct line. Each checkpoint is owned by the operator at that stage - ownership is what makes the system work without an inspection department:
| Stage | Check | Tool / method | Caught defect |
|---|---|---|---|
| Blank cutting | Squareness, dimensions, notch position | Caliper, square, first-section check | Out-of-square blanks, wrong size, misplaced notches |
| Lock forming | Seam profile, groove depth, edge condition | Profile caliper, visual under light | Shallow locks, burred edges, worn-roller marks |
| Seam closing | Seam tightness, roller pressure consistency | Leak check, feel along the seam | Uneven seams, corner leaks, buckling |
| Flanging | Flange flatness, corner fit, gasket groove | Straightedge, corner test assembly | Twisted flanges, mismatched corners |
| Assembly | Section squareness, joint alignment | Frame square, test dry-fit | Rack in the section, misaligned joints |
| Pressure test | Leakage class against spec | Test rig at rated static pressure | Seam leaks, corner leaks, flange leaks |
What Machines Decide About Quality
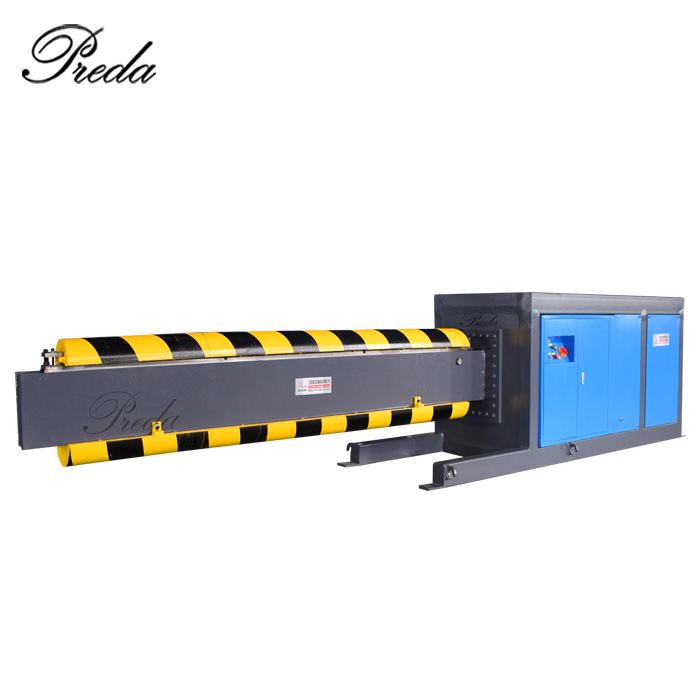
Three machine decisions set most of the quality ceiling. The first is blank squareness: a line like the AML-3 that levelers, notches and shears in one programmed pass produces blanks that are square within the machine's repeatability - the operator's job becomes verification, not correction. The second is seam consistency: a vertical hydraulic closer like the HF-1550 applies uniform roller pressure along the full length, so the section that leaves the machine is the section that passes the test, instead of depending on who swung the hammer that day. The third is profile stability on lockforming: worn rollers drift, and a drift of a few tenths of a millimetre in the lock profile is invisible on the bench and fatal at the pressure test. Machines that hold profile, and operators who check it, are the whole quality system.
Common Duct Defects, Their Causes and Where They Show Up
| Defect | Root cause | Where it is first caught |
|---|---|---|
| Out-of-square blanks | Hand cutting, loose backgauge, wrong setup | First-section check after setup |
| Corner leaks | Uneven seam closure at the corner radius | Pressure test |
| Buckled panels | No stiffening beads on long panels | Assembly, or on site under static pressure |
| Twisted flanges | Flange former out of alignment | Flanging stage, straightedge check |
| Drifting seam profile | Worn lockformer rollers | Mid-run spot check, or first leak at the test |
| Scratched galvanized | Dirty rollers, sharp tooling edges | Visual during assembly |
The Pressure Test Is the Final Judge
Every quality system ends at the same place: the section holds its leakage class at rated static pressure. The honest shop tests every section, or at minimum tests per the spec frequency and keeps the results. The pressure test is also the most expensive place to find a defect - which is why the checkpoints upstream exist. A shop that pressure-tests and records the results builds a feedback loop: a seam leak traced back to the closer tells the operator which roller to adjust; a corner leak tells the setup which pressure setting to change. The test stops being a pass/fail gate and becomes the calibration signal for the whole line.
Turning QC Data Into Setup Changes
Record the results, and the defects tell you which machine needs what. Three consecutive corner leaks point at the closer pressure setting, not at the crew. A drift in seam profile across a shift points at roller wear, not at the operator. A pattern of out-of-square blanks points at the backgauge or the shear setup. Shops that keep a simple log - date, section, defect, machine, fix - find that most recurring defects are eliminated within a month because the log makes the pattern visible. Without the log, every defect is a one-off mystery and every fix is a guess.
The first-section rule
Check the first section out of every setup and changeover with calipers - dimensions, squareness, seam profile. The thirty seconds it takes prevents a batch of scrap that would otherwise be discovered at the pressure test, ten times the cost later.
Preda Care Service Promise
Every Preda Machine ships CE certified with a two-year warranty, backed by 24/7 technical support, free spare parts shipping, remote PLC programming assistance and a global agent network. When a quality pattern points at a machine setting, the support engineer can walk the setup change with you remotely.
Build Quality Into the Machine
Ask how repeatable geometry is held on each machine - we will send specs and factory videos showing the seam and the blanks under load.
Compare Machines →Frequently Asked Questions
What are the most common duct fabrication defects?
Out-of-square blanks, corner leaks from uneven seam closure, buckled panels from missing stiffening beads, twisted flanges, and drifting seam profiles from worn rollers. All are caught early with the checkpoint system above.
How often should duct be pressure tested?
At minimum per the project spec and the applicable fabrication standard. Shops that want a feedback loop test every section - the results are what calibrate the machines upstream.
Does a better machine mean fewer defects?
Repeatable machines remove the operator-dependent variables - blank squareness and seam pressure being the two big ones. The operator still owns the checks, but the machine makes the checks pass consistently.
Where does duct quality control usually fail?
At the skipped checkpoint: the first-section check after setup is the one most shops skip, and it is the one that prevents whole batches of scrap. The second most common failure is not recording results, so patterns never become visible.