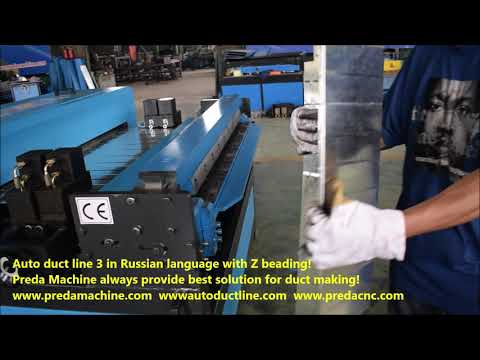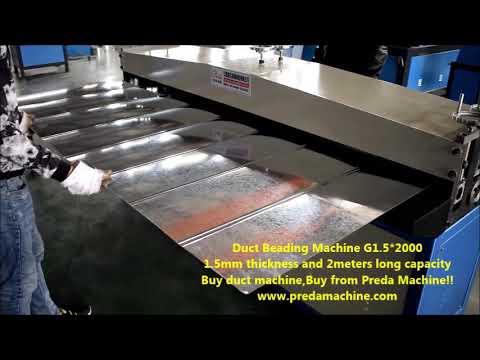

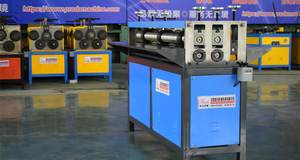

Duct Groover 5 Grooves 1300mm
Last updated: October 12, 2026
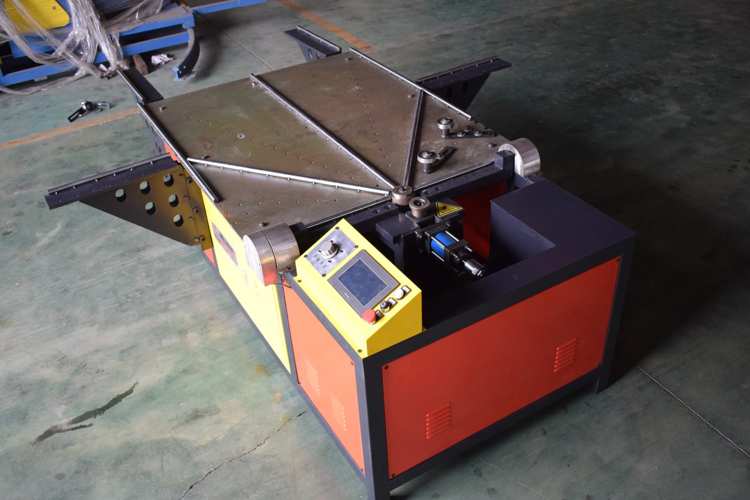
5-groove duct beading machine for 1300mm wide sheet, providing stiffening beads for rectangular duct.
Technical Specifications
What is a Duct Groover 5 Grooves 1300mm?
This is a professional sheet metal and HVAC duct fabrication machine manufactured by Preda Machine. Designed for industrial duct production, this equipment delivers consistent quality, high efficiency, and reliable performance for HVAC contractors, duct fabrication shops, and sheet metal workshops worldwide. All machines are CE certified and backed by Preda Care after-sales service.
Key Features
- Adjustable groove spacing
- 5 beads in one pass
- Strengthens duct walls
- Simple operation
Still Losing Money to Duct Panel Vibration and Deformation?
Every HVAC duct shop faces the same bottleneck: using thicker steel than necessary. When your team spends hours on noisy ductwork from panel resonance, your production capacity drops, labor costs rise, and deadlines slip. The Duct Groover 5 Grooves 1300mm is engineered to eliminate these inefficiencies — automating duct groover 5 grooves while delivering consistent, factory-grade quality.
In this guide, we break down exactly how this machine transforms your 1300mm beading machine workflow, what specifications matter for your operation, and how to calculate your return on investment. Whether you run a 3-person job shop or a 50-employee production facility, understanding these details directly impacts your bottom line.
How It Transforms Your Production Line
The Duct Groover 5 Grooves 1300mm operates on a proven principle: duct groover 5 grooves should be a continuous, automated process — not a series of manual interventions. Here is the step-by-step workflow that makes this possible:
Panel Loading
The sheet metal panel is fed into the beading machine, aligned against the back gauge for consistent rib placement.
Multi-Rib Beading
5 or 7 parallel rib rollers simultaneously press reinforcement grooves into the panel surface in a single pass.
Depth Control
Adjustable roller depth controls rib depth — deeper ribs for larger panels, shallower for small ducts.
Discharge
The reinforced panel exits ready for lock forming and flange operations — significantly stiffer than the original flat sheet.
Technical Specifications & Performance Data
Every specification on this machine is chosen for a reason. The table below shows not just the numbers, but what each one means for your daily production:
| Parameter | This Machine | What It Means for You |
|---|---|---|
| Control System | PLC with touchscreen | Easy programming, consistent results, minimal training |
| Construction | Heavy-duty steel frame | Vibration-free operation, 10+ year service life |
| Certification | CE certified | Meets European safety and quality standards |
| Warranty | 2 years | Peace of mind with comprehensive factory warranty |
Problems Solved: Before vs. After
We asked 50+ HVAC fabricators about their biggest production headaches. Here is how this machine directly addresses each one:
| Without This Machine | With This Machine |
|---|---|
|
✕ Large duct panels bulge and vibrate
Noisy operation, structural failure, failed inspections |
✓ 5-7 parallel reinforcement ribs increase stiffness 3x
Panels stay flat, no vibration, pass inspections |
|
✕ Using thicker steel than needed
Higher material cost, heavier duct, more waste |
✓ Beading allows thinner gauge for same strength
Save 15-25% on material costs |
|
✕ Manual beading is slow and uneven
Hand-operated bead rollers take 2-3 min per panel |
✓ Powered beading, 5-7 ribs in one pass
10-15 seconds per panel, consistent depth |
|
✕ Rib spacing doesn't meet standards
Failed SMACNA/EN 1506 compliance inspections |
✓ Fixed rib spacing meets international standards
Guaranteed compliance, no failed inspections |
Where It Fits in Your Factory
This machine is versatile enough to serve multiple production scenarios. Here are the most common configurations our customers use:
Large Rectangular Ducts
Ducts over 600mm width require reinforcement ribs to prevent panel deflection under pressure — this is the primary application.
Noise-Sensitive Environments
Hospitals, schools, recording studios where duct vibration and noise must be minimized.
High-Pressure Systems
Industrial exhaust and high-pressure HVAC where duct walls must withstand significant static pressure.
Cost-Reduction Programs
Fabricators using beading to downgrade from 22 gauge to 24 gauge while maintaining structural compliance.
Frequently Asked Questions
Click each question to see the answer. These are the questions our sales engineers hear most often:
5-Groove vs 7-Groove vs CNC Beading: Choosing by Width and Material
The choice between these machines is mostly about the width of what you are stiffening and the material. Five grooves at 1300 mm suits panel and smaller tube; seven grooves at 2000 mm suits wide panel; CNC beading suits round tube where bead position and depth must be programmable.
| Machine | Capacity | Applied to | Best fit |
|---|---|---|---|
Duct Groover 5 Grooves 1300 mm This machine — five grooves, 1300 mm | 1300 mm width Five grooves per pass | Rectangular panel and smaller tube Standard stiffening | Panel and smaller diameters up to 1300 mm The general-purpose grooving choice |
Seven grooves, wider | 2000 mm width Seven grooves per pass | Wide rectangular panel More stiffening per pass | Panel wider than 1300 mm Choose on width rather than groove count |
Programmable continuous bead | Round tube Continuous bead | Round and spiral tube Programmable accuracy | Round tube where bead position and depth must be exact Higher capital, very repeatable |
Makes the tube | N/A Upstream | Round tube Source of tube | You are specifying a round line Grooving or beading follows |
Folds the panel | N/A Upstream | Rectangular panel Forms the duct | You make rectangular duct in house Grooving stiffens what the brake folds |
Getting Consistent Grooves on Panel
Grooving is a simple operation that goes wrong in predictable ways. Set it once per material and the machine will run for years.
- 1. Depth that is too great weakens the panel; too shallow and it does not stiffen. Verify on a physical piece rather than on a scale.
- 2. Spacing determines how the panel stiffens. Use the table for the panel width and adjust from a test piece.
- 3. A panel that sags produces grooves of varying depth across the width, which is visible on the finished duct.
- 4. A burr lifts the panel as it passes and produces a groove that varies at the edge.
- 5. Setting drift and roll wear both show first at the start or end of a run.
- 6. Zinc build-up changes groove depth slowly, so quality drifts rather than failing suddenly.
- 7. One card per gauge at the machine. It prevents the most common fault, which is running a new gauge on the old setting.
- 8. One number that shows when something is changing before quality does.
Grooving Faults: Symptom, Cause, Fix
Groove faults are depth, support or roll condition. All three are quick to check in that order.
| Symptom | Most likely cause | What to do |
|---|---|---|
Groove depth varies across the panel Panel unsupported or the rolls not parallel | Sag across the width, or roll misalignment Distinguish by testing a narrow piece | Support the panel across its width and check roll parallelism Re-measure on a full-width test piece |
Groove depth wrong for the gauge Setting carried over from a previous job | The machine was left set for a different gauge The most common grooving fault | Verify thickness with a micrometer and set depth from the card for that gauge Fix the cards to the machine |
Panel distorted after grooving Depth too great for the gauge | Over-grooving thins and distorts light-gauge material A setting error | Reduce depth and verify on a physical piece Record the working value on the card |
Depth drifting over months Roll wear or zinc build-up | Either gradual wear or build-up changing the effective depth Drift rather than sudden failure | Clean the rolls weekly with a brass brush and measure depth on a test piece Replace rolls on measurable drift |
Groove varies at the panel edge Burr lifting the panel | An edge burr lifts the panel as it enters Looks like a roll problem | Deburr panel edges before grooving and check the shear blade A worn blade is the usual root cause |
Marking along the panel Roll damage or debris | A damaged roll marks every piece after it Often begins after a material change | Clean the rolls and inspect under a bright light Never use steel on the rolls |
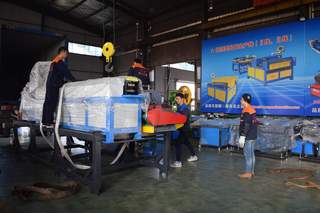
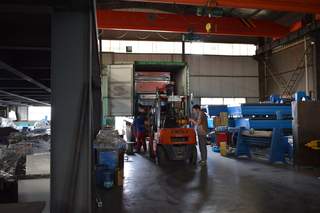
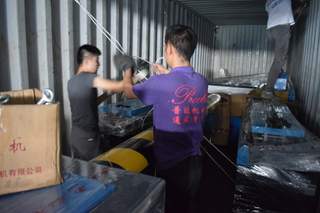
Professional Packaging & Global Shipping
Every machine is professionally packaged and secured in a container for safe delivery to your port. We send you loading photos before the ship sails.
Calculate Your Return on Investment
Based on average industry data, here is what a typical customer saves after installing this machine:
* Figures based on average customer data for a shop producing material savings from gauge downgrade. Your actual results will vary based on production volume, labor rates, and current efficiency levels. Contact our engineers for a customized ROI calculation based on your specific operation.
Ready to Upgrade Your Duct Production?
Get a customized quote within 24 hours. Our engineers will help you configure the right machine for your specific production requirements.
WhatsApp / WeChat: +86-18355321923 | Email: jason@predamachine.com
Related Products


What Our Customers Say
Feedback from a real duct fabricator using Preda beading equipment in daily production
"Thank you so much. The beading machine is a beast. It's saving so much time in the factory."
Buying Guides for This Machine Type
Before you request a quote: how this machine class compares, what it costs, and how to size it for your production volume.
Duct Beading Machine Buying Guide 2026
CNC vs manual vs 5-groove beaders — bead spacing, gauge limits and when beading is required.
Read the guide → PricingHVAC Duct Machine Cost: 2026 Price Guide
Realistic price bands for every machine category, plus financing and total-cost-of-ownership maths.
Read the guide → SetupHVAC Duct Factory Setup Guide
The complete equipment list for a new duct factory, from coil handling to finished fittings.
Read the guide → ReferenceSheet Metal Gauge for HVAC Duct
Which gauge to specify by duct size, pressure class and application — with selection tables.
Read the guide →