American Standard Pan Brake 2500mm
Last updated: October 12, 2026
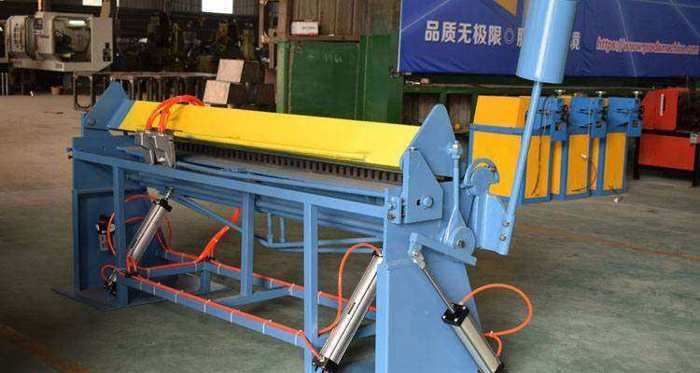
Manual pan brake (finger brake) meeting American standards for versatile box and pan forming.
Technical Specifications
What is a American Standard Pan Brake 2500mm?
This is a professional sheet metal and HVAC duct fabrication machine manufactured by Preda Machine. Designed for industrial duct production, this equipment delivers consistent quality, high efficiency, and reliable performance for HVAC contractors, duct fabrication shops, and sheet metal workshops worldwide. All machines are CE certified and backed by Preda Care after-sales service.
Key Features
- Removable finger set
- Adjustable clamping force
- Precision angle indicator
- Heavy-duty steel frame
Still Losing Money to Inaccurate Bends and Wasted Material?
Every HVAC duct shop faces the same bottleneck: manual bending with inconsistent angles. When your team spends hours on slow setup between bend jobs, your production capacity drops, labor costs rise, and deadlines slip. The American Standard Pan Brake 2500mm is engineered to eliminate these inefficiencies — automating American standard pan brake while delivering consistent, factory-grade quality.
In this guide, we break down exactly how this machine transforms your 2500mm finger brake workflow, what specifications matter for your operation, and how to calculate your return on investment. Whether you run a 3-person job shop or a 50-employee production facility, understanding these details directly impacts your bottom line.
How It Transforms Your Production Line
The American Standard Pan Brake 2500mm operates on a proven principle: American standard pan brake should be a continuous, automated process — not a series of manual interventions. Here is the step-by-step workflow that makes this possible:
Material Positioning
The sheet is positioned against the back gauge, which controls the bend line location with precision accuracy.
Clamping
The clamping beam secures the sheet firmly, preventing any movement during the bending cycle.
Precision Bending
The bending beam or ram applies controlled force to bend the metal to the programmed angle — CNC models achieve ±0.2° accuracy.
Release & Reposition
The clamp releases, the sheet is repositioned for the next bend, and the cycle repeats — multi-bend parts are completed in seconds.
Technical Specifications & Performance Data
Every specification on this machine is chosen for a reason. The table below shows not just the numbers, but what each one means for your daily production:
| Parameter | This Machine | What It Means for You |
|---|---|---|
| Control System | PLC with touchscreen | Easy programming, consistent results, minimal training |
| Construction | Heavy-duty steel frame | Vibration-free operation, 10+ year service life |
| Certification | CE certified | Meets European safety and quality standards |
| Warranty | 2 years | Peace of mind with comprehensive factory warranty |
Problems Solved: Before vs. After
We asked 50+ HVAC fabricators about their biggest production headaches. Here is how this machine directly addresses each one:
| Without This Machine | With This Machine |
|---|---|
|
✕ Inconsistent bend angles
Parts don't fit together, rework rate 10-15% |
✓ CNC angle control ±0.2° repeatability
Every bend identical, zero rework |
|
✕ Slow manual bending
Hand brakes take 2-3 minutes per bend |
✓ Powered/CNC bending, 5-10 seconds per bend
10-20x faster throughput |
|
✕ Limited bend complexity
Can only do simple 90° bends by hand |
✓ Multi-axis CNC with programmable bend sequences
Complex boxes, pans, and profiles in one setup |
|
✕ Operator fatigue and injury
Heavy manual lifting causes strains and injuries |
✓ Powered clamping and bending
Reduced physical strain, safer workplace |
Where It Fits in Your Factory
This machine is versatile enough to serve multiple production scenarios. Here are the most common configurations our customers use:
Rectangular Duct Fittings
Bending duct panels into L-shapes, U-shapes, and complete rectangular forms — the core application in HVAC fabrication.
Flange & Connector Parts
Bending TDF flange corners, drive cleats, S-slips, and other duct connection components.
Custom Sheet Metal
Architectural metalwork, equipment enclosures, brackets, and custom fabrication jobs.
General Manufacturing
Any industry requiring precision sheet metal bending — from automotive to electronics enclosures.
Frequently Asked Questions
Click each question to see the answer. These are the questions our sales engineers hear most often:
Pan Brake: Choosing Between Manual, Hydraulic and CNC Folding
A pan brake folds straight bends in long sheet — boxes, pans, and the straight folds that a rolling machine cannot make. At 2500 mm width the question is not whether you need one, but how much of the setting you want the machine to do for you.
| Option | Repeatability | Set-up | Best fit |
|---|---|---|---|
American Standard Pan Brake 2500 mm This machine — manual folding | Good, operator-dependent Set the stop and fold | Fast for simple folds No programming | Job-shop work with varied folds and moderate volume Also the right choice where a CNC brake would be idle capacity |
Curves, not folds | N/A Different shape | N/A Not comparable | You need curves rather than straight folds Many shops need both machines |
Curves with pre-bending | N/A Curves | N/A Not comparable | Curved work where the flat end is unacceptable Not an alternative to folding |
Cuts the blank | High Programmed | Upstream of folding Prepares blanks | You need accurate blanks before folding Blank accuracy determines fold accuracy |
Dedicated cleats | Very high Set once | Specialised One profile | Cleats are regular rather than occasional Frees the brake for other work |
Getting Straight, Repeatable Folds at 2.5 m
Long sheet amplifies every error: a blank that is a degree out of square produces a box that will not close. These steps keep long folds accurate.
- 1. Measure both diagonals. At 2.5 m, a diagonal difference of 2 mm is enough to make a box that will not close.
- 2. Bend allowance varies with gauge and material. Use the table, and verify on a test fold before running the batch.
- 3. A back stop is the difference between repeatable and approximate. Set it and check it at the start of each batch.
- 4. At 2.5 m the sheet will sag and the fold line will not be straight. Support it, or use a second operator on long work.
- 5. One test fold costs a minute and prevents a batch of parts that do not assemble.
- 6. Overbend slightly to compensate. The amount depends on material and gauge — record it rather than estimating each time.
- 7. Debris on the beam produces a fold line that is not straight, which is visible on the finished part.
- 8. Parts with four folds take four times as long. Log by folds, not by parts, to get an honest picture of capacity.
Pan Brake Faults: Symptom, Cause, Fix
Fold faults are nearly always blank accuracy, stop setting or springback. Check in that order.
| Symptom | Most likely cause | What to do |
|---|---|---|
Box will not close Blank out of square or bend allowance wrong | Accumulated error from a blank that is not square, or a wrong allowance At 2.5 m the error is amplified four times on a four-sided box | Check both diagonals on the blank and verify the bend allowance on a test fold Square the shear before blaming the brake |
Fold angle inconsistent Springback not compensated, or the material varies | Different gauge or material springs back differently Often a material change rather than a machine issue | Record the overbend for each gauge and material and use the recorded value Re-check when the material changes |
Fold line not straight Sheet unsupported or the beam contaminated | Sag along the length, or debris under the clamp Common on long work with one operator | Support the sheet along its length and clean the beam and clamp Use a second operator on full-width work |
Flange width varies Back stop not set or has moved | No positive stop, or it has worked loose The most common cause of variable flanges | Set the back stop and check it at the start of every batch Add it to the weekly inspection |
Material marks at the fold Clamp pressure too high or the beam edge damaged | Excessive clamp pressure marks soft material, and a damaged beam edge marks everything Distinguish by looking at the beam | Reduce clamp pressure to the minimum that holds the sheet and inspect the beam edge Clean the beam before every job |
Machine will not fold the specified gauge At the capacity limit for the width | Capacity is thickness times width — full width reduces the thickness you can fold A specification boundary rather than a fault | Check thickness and width against the capacity chart Never exceed the rating — it damages the beam and the clamp |
Professional Packaging & Global Shipping
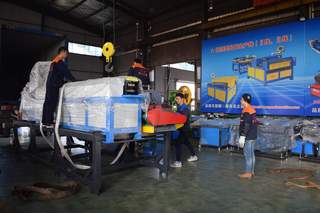
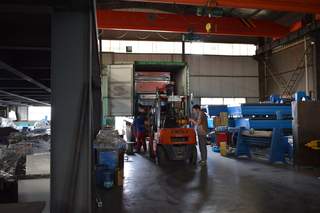
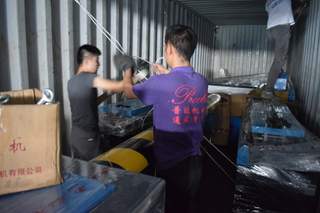
Every machine is professionally packaged and secured in a container for safe delivery to your port. We send you loading photos before the ship sails.
Calculate Your Return on Investment
Based on average industry data, here is what a typical customer saves after installing this machine:
* Figures based on average customer data for a shop producing 100-500 bends per day. Your actual results will vary based on production volume, labor rates, and current efficiency levels. Contact our engineers for a customized ROI calculation based on your specific operation.
Ready to Upgrade Your American Production?
Get a customized quote within 24 hours. Our engineers will help you configure the right machine for your specific production requirements.
WhatsApp / WeChat: +86-18355321923 | Email: jason@predamachine.com
Related Products

Buying Guides for This Machine Type
Before you request a quote: how this machine class compares, what it costs, and how to size it for your production volume.
Sheet Metal Bending Machine Guide 2026
Press brake vs pan brake vs roller bender for ductwork and fittings production.
Read the guide → SizingHydraulic Press Brake for HVAC
How to size tonnage and bed length for duct shop work without overbuying capacity.
Read the guide → ReferenceSheet Metal Brake Types
Press brake, pan brake and box-and-pan folder explained — strengths, limits and typical jobs.
Read the guide → PricingHVAC Duct Machine Cost: 2026 Price Guide
Realistic price bands for every machine category, plus financing and total-cost-of-ownership maths.
Read the guide →