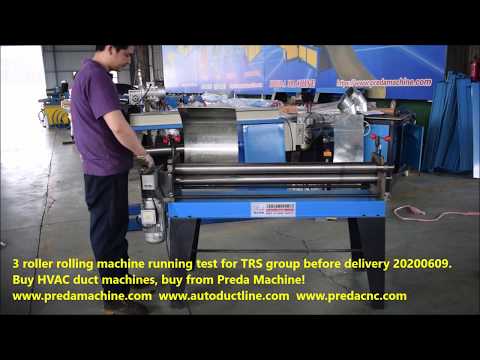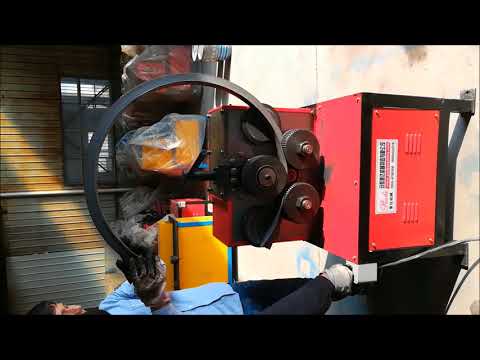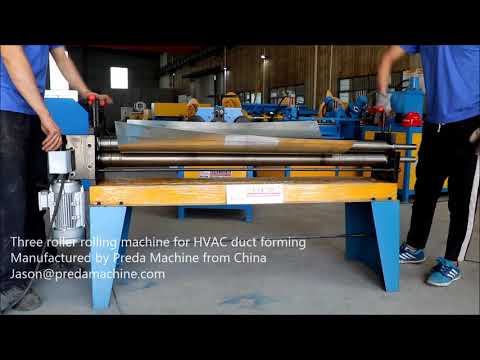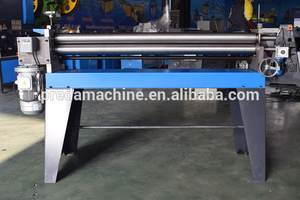
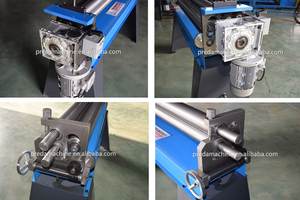


4-Roller Plate Rolling Machine W12-4×2000
Last updated: October 12, 2026
Four-roller plate rolling machine for high-precision cylindrical and conical forming. CNC control with automatic pre-bending and rolling.
Technical Specifications
What is a 4-Roller Plate Rolling Machine W12-4×2000?
A sheet metal bending machine (also called a press brake or folder) is a machine tool that bends sheet metal into precise angles and shapes. In HVAC duct fabrication, bending machines create the folded edges, seams, and connector profiles needed for rectangular duct assembly. CNC press brakes offer programmable angle control and backgauge positioning for high-volume production, while manual folders suit smaller shops and custom work.
Key Features
- 4-roller precision rolling
- CNC control available
- Automatic pre-bending
- Cylindrical and conical shapes
- High precision
- Heavy-duty construction
Still Losing Money to Inaccurate Bends and Wasted Material?
Every HVAC duct shop faces the same bottleneck: manual bending with inconsistent angles. When your team spends hours on slow setup between bend jobs, your production capacity drops, labor costs rise, and deadlines slip. The 4-Roller Plate Rolling Machine W12-4×2000 is engineered to eliminate these inefficiencies — automating 4 roller plate rolling machine while delivering consistent, factory-grade quality.
In this guide, we break down exactly how this machine transforms your W12 CNC rolling workflow, what specifications matter for your operation, and how to calculate your return on investment. Whether you run a 3-person job shop or a 50-employee production facility, understanding these details directly impacts your bottom line.
How It Transforms Your Production Line
The 4-Roller Plate Rolling Machine W12-4×2000 operates on a proven principle: 4 roller plate rolling machine should be a continuous, automated process — not a series of manual interventions. Here is the step-by-step workflow that makes this possible:
Material Positioning
The sheet is positioned against the back gauge, which controls the bend line location with precision accuracy.
Clamping
The clamping beam secures the sheet firmly, preventing any movement during the bending cycle.
Precision Bending
The bending beam or ram applies controlled force to bend the metal to the programmed angle — CNC models achieve ±0.2° accuracy.
Release & Reposition
The clamp releases, the sheet is repositioned for the next bend, and the cycle repeats — multi-bend parts are completed in seconds.
Technical Specifications & Performance Data
Every specification on this machine is chosen for a reason. The table below shows not just the numbers, but what each one means for your daily production:
| Parameter | This Machine | What It Means for You |
|---|---|---|
| Control System | PLC with touchscreen | Easy programming, consistent results, minimal training |
| Construction | Heavy-duty steel frame | Vibration-free operation, 10+ year service life |
| Certification | CE certified | Meets European safety and quality standards |
| Warranty | 2 years | Peace of mind with comprehensive factory warranty |
Problems Solved: Before vs. After
We asked 50+ HVAC fabricators about their biggest production headaches. Here is how this machine directly addresses each one:
| Without This Machine | With This Machine |
|---|---|
|
✕ Inconsistent bend angles
Parts don't fit together, rework rate 10-15% |
✓ CNC angle control ±0.2° repeatability
Every bend identical, zero rework |
|
✕ Slow manual bending
Hand brakes take 2-3 minutes per bend |
✓ Powered/CNC bending, 5-10 seconds per bend
10-20x faster throughput |
|
✕ Limited bend complexity
Can only do simple 90° bends by hand |
✓ Multi-axis CNC with programmable bend sequences
Complex boxes, pans, and profiles in one setup |
|
✕ Operator fatigue and injury
Heavy manual lifting causes strains and injuries |
✓ Powered clamping and bending
Reduced physical strain, safer workplace |
Where It Fits in Your Factory
This machine is versatile enough to serve multiple production scenarios. Here are the most common configurations our customers use:
Rectangular Duct Fittings
Bending duct panels into L-shapes, U-shapes, and complete rectangular forms — the core application in HVAC fabrication.
Flange & Connector Parts
Bending TDF flange corners, drive cleats, S-slips, and other duct connection components.
Custom Sheet Metal
Architectural metalwork, equipment enclosures, brackets, and custom fabrication jobs.
General Manufacturing
Any industry requiring precision sheet metal bending — from automotive to electronics enclosures.
Frequently Asked Questions
Click each question to see the answer. These are the questions our sales engineers hear most often:
4-Roller: What the Fourth Roll Buys You
The fourth roll pre-bends the sheet edge, which removes the flat end that a 3-roller leaves behind. That is the whole point of the machine, and it is worth the premium only when the flat end costs you real money — in material trim, in a second operation, or in rework.
| Machine | Pre-bending | Flat end | Verdict |
|---|---|---|---|
4-Roller Plate Rolling Machine W12-4×2000 This machine — four rolls, integrated pre-bend | Yes — the sheet edge is pre-bent in the same set-up One pass, no separate operation | Effectively none The reason to buy this machine | The flat end is costing you material or a second operation Or accuracy requirements rule it out |
Three rolls, no pre-bend | No — pre-bending must be done separately Or the flat is trimmed off | Roughly half the lower roll spacing at each end Acceptable or trimmable in many jobs | The flat end can be trimmed or designed around Lower capital and simpler to run |
Straight folds, not curves | N/A Different shape | N/A Not comparable | You need straight folds rather than curves Often bought alongside a roller, not instead of it |
Cleats and small profiles | N/A Specialised | N/A Dedicated machine | You make drive cleats routinely Not a substitute for rolling capacity |
Cuts the blank | N/A Upstream of rolling | N/A Prepares the sheet | You need blanks cut square before rolling A square blank is a prerequisite for a true cylinder |
Setting Up a 4-Roller for Repeatable Work
A 4-roller has one more setting than a 3-roller and one more way to be wrong. Standardise the sequence and the machine is faster per piece than any alternative.
- 1. A blank that is out of square cannot produce a true cylinder regardless of the machine. Check the diagonal measurements before rolling.
- 2. Sequence matters. Pre-bend sets the edge; the main bend then forms the body. Doing it in the other order produces an inconsistent edge.
- 3. As on any rolling machine, tighten gradually. You cannot un-bend a sheet.
- 4. Two variables determine the radius, and both need recording. Fix the cards to the machine.
- 5. The pre-bend is the reason you bought this machine. Check it explicitly rather than assuming.
- 6. Four rolls must be parallel. Misalignment shows as a radius that varies across the width of the sheet.
- 7. At 2 m width the sheet needs support along its length or it will drop and produce a varying radius.
- 8. You need this number to know whether the premium was justified, and it is usually better than expected because the second operation disappears.
4-Roller Faults: Symptom, Cause, Fix
Four rolls mean parallelism matters. Most faults that look like radius problems are alignment problems.
| Symptom | Most likely cause | What to do |
|---|---|---|
Radius varies across the sheet width Rolls not parallel | Misalignment between the rolls produces a tapered radius The most common 4-roller-specific fault | Check roll parallelism across the width and re-set per the manual Check monthly as preventive maintenance |
Edge not properly pre-bent Side roll setting or sequence wrong | The pre-bend was set after the main bend, or the side roll is not far enough A sequence error in most cases | Set the side roll first, then the main bend, and verify on the first piece Write the sequence on the set-up card |
Cylinder has a seam gap Blank out of square or wrong developed length | The blank geometry, not the rolling Easy to misdiagnose as a machine fault | Check the blank diagonals and the developed length before rolling Square and deburr blanks as standard |
Surface marking Roll damage or debris | A damaged roll marks every piece that follows Usually traced to swarf or a damaged sheet edge | Clean the rolls with a brass brush and deburr blanks Never use steel on the roll surface |
Sheet slips during pre-bending Side roll grip insufficient | The pre-bend takes the most grip of any stage Common on thicker material or contaminated rolls | Degrease the rolls and check the side roll pressure for the gauge Confirm the material is inside the specified capacity |
Machine labours at full width At the limit of the capacity envelope | Capacity is thickness times width — full width reduces the thickness you can roll A specification boundary, not a fault | Check the thickness and width against the capacity chart Reduce width or thickness rather than forcing it |
Professional Packaging & Global Shipping
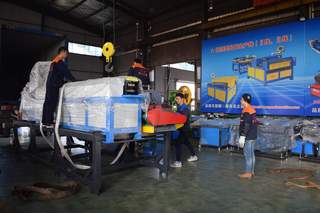
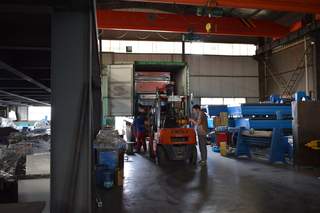
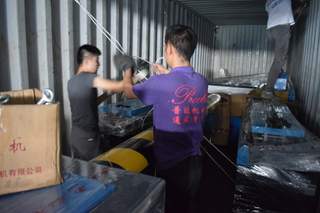
Every machine is professionally packaged and secured in a container for safe delivery to your port. We send you loading photos before the ship sails.
Calculate Your Return on Investment
Based on average industry data, here is what a typical customer saves after installing this machine:
* Figures based on average customer data for a shop producing 100-500 bends per day. Your actual results will vary based on production volume, labor rates, and current efficiency levels. Contact our engineers for a customized ROI calculation based on your specific operation.
Ready to Upgrade Your 4-Roller Production?
Get a customized quote within 24 hours. Our engineers will help you configure the right machine for your specific production requirements.
WhatsApp / WeChat: +86-18355321923 | Email: jason@predamachine.com
Related Products

Buying Guides for This Machine Type
Before you request a quote: how this machine class compares, what it costs, and how to size it for your production volume.
Sheet Metal Bending Machine Guide 2026
Press brake vs pan brake vs roller bender for ductwork and fittings production.
Read the guide → SizingHydraulic Press Brake for HVAC
How to size tonnage and bed length for duct shop work without overbuying capacity.
Read the guide → ReferenceSheet Metal Brake Types
Press brake, pan brake and box-and-pan folder explained — strengths, limits and typical jobs.
Read the guide → PricingHVAC Duct Machine Cost: 2026 Price Guide
Realistic price bands for every machine category, plus financing and total-cost-of-ownership maths.
Read the guide →