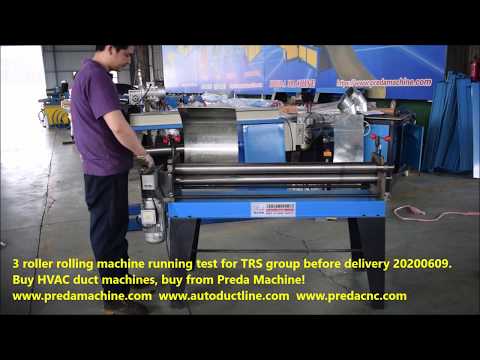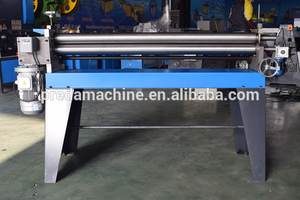
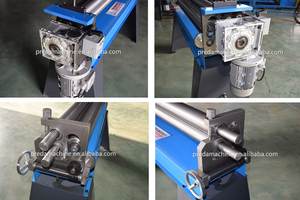


3 Roller Bending Machine
Last updated: October 12, 2026
Three-roller plate rolling machine for forming cylindrical and conical shapes from sheet metal.
Technical Specifications
What is a 3 Roller Bending Machine?
A sheet metal bending machine (also called a press brake or folder) is a machine tool that bends sheet metal into precise angles and shapes. In HVAC duct fabrication, bending machines create the folded edges, seams, and connector profiles needed for rectangular duct assembly. CNC press brakes offer programmable angle control and backgauge positioning for high-volume production, while manual folders suit smaller shops and custom work.
Key Features
- Asymmetric 3-roller design
- Pre-bending capability
- Manual or electric adjustment
- Versatile rolling applications
Still Losing Money to Inaccurate Bends and Wasted Material?
Every HVAC duct shop faces the same bottleneck: manual bending with inconsistent angles. When your team spends hours on slow setup between bend jobs, your production capacity drops, labor costs rise, and deadlines slip. The 3 Roller Bending Machine is engineered to eliminate these inefficiencies — automating 3 roller bending machine while delivering consistent, factory-grade quality.
In this guide, we break down exactly how this machine transforms your plate rolling machine workflow, what specifications matter for your operation, and how to calculate your return on investment. Whether you run a 3-person job shop or a 50-employee production facility, understanding these details directly impacts your bottom line.
How It Transforms Your Production Line
The 3 Roller Bending Machine operates on a proven principle: 3 roller bending machine should be a continuous, automated process — not a series of manual interventions. Here is the step-by-step workflow that makes this possible:
Material Positioning
The sheet is positioned against the back gauge, which controls the bend line location with precision accuracy.
Clamping
The clamping beam secures the sheet firmly, preventing any movement during the bending cycle.
Precision Bending
The bending beam or ram applies controlled force to bend the metal to the programmed angle — CNC models achieve ±0.2° accuracy.
Release & Reposition
The clamp releases, the sheet is repositioned for the next bend, and the cycle repeats — multi-bend parts are completed in seconds.
Technical Specifications & Performance Data
Every specification on this machine is chosen for a reason. The table below shows not just the numbers, but what each one means for your daily production:
| Parameter | This Machine | What It Means for You |
|---|---|---|
| Control System | PLC with touchscreen | Easy programming, consistent results, minimal training |
| Construction | Heavy-duty steel frame | Vibration-free operation, 10+ year service life |
| Certification | CE certified | Meets European safety and quality standards |
| Warranty | 2 years | Peace of mind with comprehensive factory warranty |
Problems Solved: Before vs. After
We asked 50+ HVAC fabricators about their biggest production headaches. Here is how this machine directly addresses each one:
| Without This Machine | With This Machine |
|---|---|
|
✕ Inconsistent bend angles
Parts don't fit together, rework rate 10-15% |
✓ CNC angle control ±0.2° repeatability
Every bend identical, zero rework |
|
✕ Slow manual bending
Hand brakes take 2-3 minutes per bend |
✓ Powered/CNC bending, 5-10 seconds per bend
10-20x faster throughput |
|
✕ Limited bend complexity
Can only do simple 90° bends by hand |
✓ Multi-axis CNC with programmable bend sequences
Complex boxes, pans, and profiles in one setup |
|
✕ Operator fatigue and injury
Heavy manual lifting causes strains and injuries |
✓ Powered clamping and bending
Reduced physical strain, safer workplace |
Where It Fits in Your Factory
This machine is versatile enough to serve multiple production scenarios. Here are the most common configurations our customers use:
Rectangular Duct Fittings
Bending duct panels into L-shapes, U-shapes, and complete rectangular forms — the core application in HVAC fabrication.
Flange & Connector Parts
Bending TDF flange corners, drive cleats, S-slips, and other duct connection components.
Custom Sheet Metal
Architectural metalwork, equipment enclosures, brackets, and custom fabrication jobs.
General Manufacturing
Any industry requiring precision sheet metal bending — from automotive to electronics enclosures.
Frequently Asked Questions
Click each question to see the answer. These are the questions our sales engineers hear most often:
3-Roller vs 4-Roller vs Press Brake: Which Bending Machine You Need
These three machines bend sheet, and they are constantly confused with one another. A 3-roller produces curves and cylinders, a 4-roller does the same with better edge control and pre-bending, and a pan brake or press brake produces straight folds. Buy on the shape you need, not on the word "bending".
| Machine | Produces | Edge control | Best fit |
|---|---|---|---|
3 Roller Bending Machine This machine — curves and cylinders | Curved panels, cylinders, swept elbows Continuous radius | A flat remains at both ends of the sheet Requires pre-bending or a second pass | Round and curved work where a flat end can be trimmed or is acceptable The standard, lower-cost rolling option |
Curves with pre-bending | Curves and cylinders Continuous radius | Pre-bends the sheet edge, so no flat end Better accuracy and one-pass operation | Curved work where the flat end is unacceptable or accuracy matters Higher capital, faster per piece |
Straight folds | Boxes, pans, straight bends Not curves | N/A A different shape entirely | You need straight folds on long sheet Often bought alongside a roller, not instead of it |
Cleats and small profiles | Drive cleats and small sections Purpose-built | N/A Specialised | You make drive cleats routinely A dedicated machine beats improvising on a brake |
Background reading | Guide, not a machine Comparison across all three types | N/A Reference | You have not decided yet Read this before comparing quotations |
Getting Accurate Curves From a 3-Roller
The flat end is the defining limitation of a 3-roller. Everything below is about managing it and about setting the roll gap repeatably.
- 1. A 3-roller leaves a flat section at each end of the sheet, roughly equal to half the distance between the lower rolls. Either trim it, design around it, or pre-bend it in a separate operation.
- 2. Form a test piece, measure the radius, adjust, and repeat. Set by feel and you will produce a morning of scrap.
- 3. It is easy to tighten a roll and hard to un-bend a sheet. Work toward the radius in small steps.
- 4. Radius depends on both. One card per radius-and-gauge pair, fixed to the machine.
- 5. A sheet fed at an angle produces a cone rather than a cylinder. Use the side guide and check the first piece.
- 6. A damaged roll marks every piece that follows and is far more expensive to fix than to prevent.
- 7. Unsupported sheet drops as it enters and produces a radius that varies along the piece.
- 8. A curved panel can measure correct at the ends and be wrong in the middle. A template shows the true shape.
3-Roller Faults: Symptom, Cause, Fix
Rolling faults are almost always radius setting, feed angle or roll condition. All three are quick to check before you change anything.
| Symptom | Most likely cause | What to do |
|---|---|---|
Flat section at each end of the sheet Inherent to a 3-roller | The flat is roughly half the distance between the lower rolls Not a fault — a characteristic of the machine | Trim it, design around it, pre-bend, or move to a 4-roller A 4-roller pre-bends the edge and removes the flat |
Cone produced instead of a cylinder Sheet fed at an angle to the rolls | The feed was not square, so one end is rolled tighter The classic 3-roller geometry fault | Use the side guide and check the first piece at both ends Re-square the feed before running the batch |
Radius varies along the piece Roll gap not stable or the sheet unsupported | Either the setting drifted during the pass or the sheet dropped at the infeed Shows as a radius that changes along the length | Support the sheet and re-set the gap, then check with a template Re-check the gap after the first few pieces |
Surface marking on the sheet Roll damage or debris | A damaged roll or a piece of swarf rolled into the surface Marks every subsequent piece | Clean the rolls with a brass brush and inspect under a bright light Never use steel on the roll surface |
Sheet slips and will not feed Roll gap too loose or the rolls contaminated | Insufficient grip, often from oil or a gap set for a thicker gauge Common after a gauge change | Tighten the gap to the recorded value for that gauge and degrease the rolls Do not feed by hand — use the drive |
Machine labours on heavy gauge Material above the specified capacity | Rollers are rated for a thickness times width envelope A specification issue rather than a fault | Verify thickness and width against the capacity chart in the manual Do not force oversize material — it damages the rolls and the drive |
Professional Packaging & Global Shipping
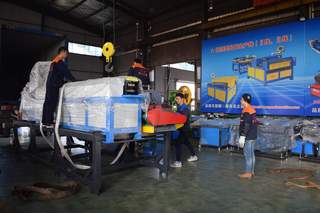
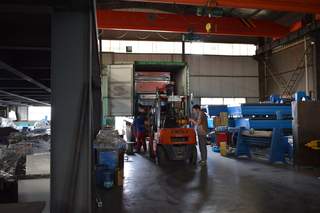
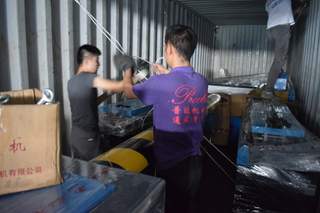
Every machine is professionally packaged and secured in a container for safe delivery to your port. We send you loading photos before the ship sails.
Calculate Your Return on Investment
Based on average industry data, here is what a typical customer saves after installing this machine:
* Figures based on average customer data for a shop producing 100-500 bends per day. Your actual results will vary based on production volume, labor rates, and current efficiency levels. Contact our engineers for a customized ROI calculation based on your specific operation.
Ready to Upgrade Your 3 Production?
Get a customized quote within 24 hours. Our engineers will help you configure the right machine for your specific production requirements.
WhatsApp / WeChat: +86-18355321923 | Email: jason@predamachine.com
Related Products

Buying Guides for This Machine Type
Before you request a quote: how this machine class compares, what it costs, and how to size it for your production volume.
Sheet Metal Bending Machine Guide 2026
Press brake vs pan brake vs roller bender for ductwork and fittings production.
Read the guide → SizingHydraulic Press Brake for HVAC
How to size tonnage and bed length for duct shop work without overbuying capacity.
Read the guide → ReferenceSheet Metal Brake Types
Press brake, pan brake and box-and-pan folder explained — strengths, limits and typical jobs.
Read the guide → PricingHVAC Duct Machine Cost: 2026 Price Guide
Realistic price bands for every machine category, plus financing and total-cost-of-ownership maths.
Read the guide →