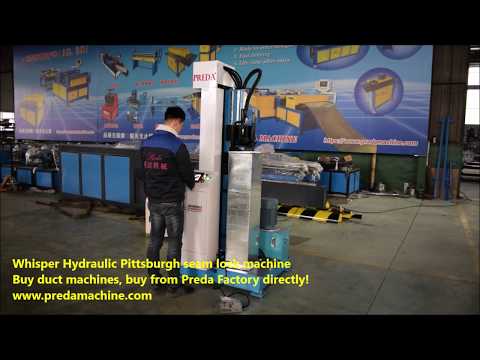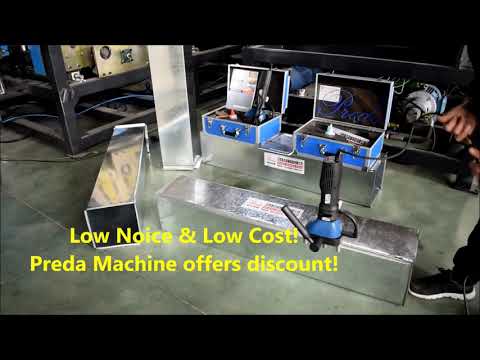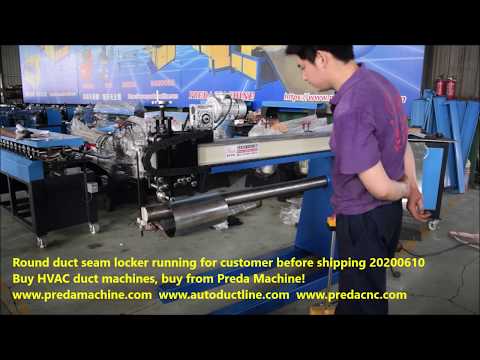


Pittsburgh Seam Locker L-12
Last updated: October 12, 2026
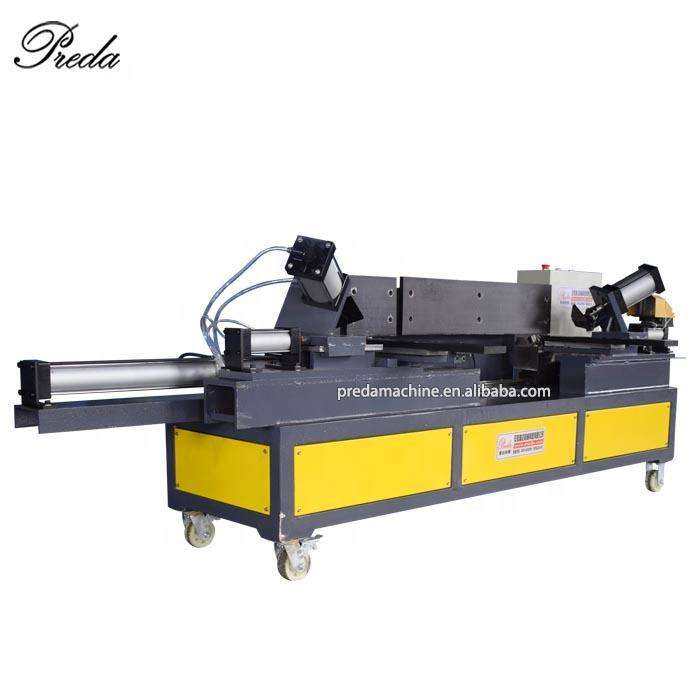
Compact Pittsburgh seam locker for closing longitudinal seams on rectangular duct, affordable entry-level solution.
Technical Specifications
What is a Pittsburgh Seam Locker L-12?
A Pittsburgh lockformer (also called a Pittsburgh lock machine or pittsburgh machine) is a sheet metal forming machine that creates the Pittsburgh lock seam — the most widely used connection method for rectangular HVAC ductwork. The machine rolls a female pocket on one edge of the sheet and a male flange on the mating edge, allowing ducts to be assembled by simply inserting and hammering the seam closed. Pittsburgh lockformers are essential equipment in any sheet metal duct fabrication shop.
Key Features
- Affordable entry-level seam closing
- Compact bench-top design
- Adjustable seam pressure
- Easy roller adjustment
- Lightweight and portable
Still Losing Money to Leaky Seams and Slow Assembly?
Every HVAC duct shop faces the same bottleneck: hammering seams closed by hand. When your team spends hours on inconsistent weld quality, your production capacity drops, labor costs rise, and deadlines slip. The Pittsburgh Seam Locker L-12 is engineered to eliminate these inefficiencies — automating pittsburgh seam locker L-12 while delivering consistent, factory-grade quality.
In this guide, we break down exactly how this machine transforms your compact seam closer workflow, what specifications matter for your operation, and how to calculate your return on investment. Whether you run a 3-person job shop or a 50-employee production facility, understanding these details directly impacts your bottom line.
How It Transforms Your Production Line
The Pittsburgh Seam Locker L-12 operates on a proven principle: pittsburgh seam locker L-12 should be a continuous, automated process — not a series of manual interventions. Here is the step-by-step workflow that makes this possible:
Seam Alignment
The Pittsburgh lock is hooked together and positioned in the seam closing machine, or the weld joint is aligned for welding.
Automatic Closing/Welding
Powered rollers close the seam along the full length, or welding electrodes create a continuous or spot weld — no manual hammering required.
Quality Check
The closed seam or weld is inspected for completeness and airtightness — consistent quality every time.
Discharge
The finished duct section is ready for flange installation and shipping.
Technical Specifications & Performance Data
Every specification on this machine is chosen for a reason. The table below shows not just the numbers, but what each one means for your daily production:
| Parameter | This Machine | What It Means for You |
|---|---|---|
| Control System | PLC with touchscreen | Easy programming, consistent results, minimal training |
| Construction | Heavy-duty steel frame | Vibration-free operation, 10+ year service life |
| Certification | CE certified | Meets European safety and quality standards |
| Warranty | 2 years | Peace of mind with comprehensive factory warranty |
Problems Solved: Before vs. After
We asked 50+ HVAC fabricators about their biggest production headaches. Here is how this machine directly addresses each one:
| Without This Machine | With This Machine |
|---|---|
|
✕ Hand hammering is slow and noisy
5-10 minutes per seam, worker fatigue, noise pollution |
✓ Powered seam closing in 10-30 seconds
10-20x faster, quiet operation, less fatigue |
|
✕ Inconsistent seam closure
Some seams leak, failed pressure tests |
✓ Uniform roller pressure along full length
Every seam identical, guaranteed airtight |
|
✕ Spot welding burns through thin metal
Holes in duct, rework and scrap |
✓ Precise current and time control
Perfect welds every time, no burn-through |
|
✕ Welding requires skilled labor
Hard to find qualified welders, high wages |
✓ Simple operation, minimal training needed
Any operator can produce quality welds |
Where It Fits in Your Factory
This machine is versatile enough to serve multiple production scenarios. Here are the most common configurations our customers use:
Pittsburgh Seam Closing
Closing the longitudinal seam on rectangular ducts after lock forming — the most common application in HVAC fabrication.
Spot Welding
Fast, clean spot welds for round duct assembly, flange attachment, and bracket installation — no filler material needed.
Seam Welding
Continuous or stitch welding for high-pressure ducts, stainless steel ducts, and applications requiring maximum airtightness.
Flange Fastening
Power fastening of TDC flange clips and connectors — faster and more consistent than manual screwdriving.
Frequently Asked Questions
Click each question to see the answer. These are the questions our sales engineers hear most often:
L-12 Seam Locker: Where It Fits in a Rectangular Line
The L-12 closes a Pittsburgh seam that has already been formed. It is the machine you add when closing has become the bottleneck on a lockformer, or when you want to run forming and closing at different rates.
| Machine | Role | Gauge | Best fit |
|---|---|---|---|
Pittsburgh Seam Locker L-12 This machine — closing only | Closes a pre-formed Pittsburgh seam Dedicated | Standard commercial gauge 24–22 ga | Closing is the bottleneck on your current lockformer Or you want forming and closing at different stations |
Forms and closes in one pass | Both operations Combined | Up to 1.0 mm One handling | You would rather keep one machine and one handling Simpler, but the pass rate is shared |
Forms and closes, heavier gauge | Both operations Combined | Up to 1.2 mm Heavier duty | Heavier gauge with one handling Step up rather than adding a separate closer |
Mechanical closing | Closing only Comparable | Standard gauge Comparable | You are comparing mechanical closers Decide on throughput and service |
Hydraulic closing | Closing only Heavier gauge | Heavier gauge Hydraulic force | You work at the heavier end of the gauge range Or seam leakage has been a recurring problem |
Setting Up the L-12 So Closing Stops Being the Bottleneck
Adding a separate closer only helps if it actually runs faster than the combined pass. Set it up to do that.
- 1. You need a baseline. Without it you cannot tell whether separating the operations actually helped.
- 2. The closer finishes; it does not form. An upstream fault survives the closer.
- 3. One setting per gauge. This is the habit that prevents most seam faults.
- 4. Ten seconds. The alternative is a batch that leaks on site.
- 5. The only reliable check, and cheap at this frequency.
- 6. An unsupported section twists and produces a seam tight at one end and open at the other.
- 7. Zinc build-up changes geometry slowly and invisibly.
- 8. Two numbers tell you whether the separation achieved what you intended.
L-12 Faults: Symptom, Cause, Fix
As with any closer, work backwards: edge condition, then forming, then closing.
| Symptom | Most likely cause | What to do |
|---|---|---|
Seam leaks Closing pressure insufficient for the gauge | Looks closed and is not The fault that reaches site | Increase pressure for the gauge and air-test a section Record the setting once it passes |
Seam tight at one end, open at the other Section unsupported and twisting | Handling rather than setting Distinguish by testing a short section | Support the section at both ends and re-check Confirm the strip edge is square |
Lock will not start Strip edge burred or out of square | Edge condition, traced to the shear in most cases Looks like a machine fault | Deburr and square the edge and check the shear blade Never force the section |
Quality drifts gradually Zinc build-up in the closing head | Slow build-up changing geometry Drift rather than sudden failure | Clean the head weekly with a brass brush, never steel Inspect under a bright light |
Throughput no better than the combined machine Feeding or stacking is the real constraint | The closer waits for sections, or finished sections pile up Common when the separation was not measured | Time both stations for a shift before investing further Add handling support rather than machine speed |
Marking along the seam Head damage or debris | A damaged head marks every metre after it Often begins after a blade change | Clean and inspect the closing head Never use steel on working surfaces |
Three Ways to Lay Out Forming and Closing
Adding a separate closing machine is a layout decision as much as a machine decision. These are the three arrangements that work, and the one that usually does not.
| Layout | How it works | Advantage | Watch out for |
|---|---|---|---|
Combined — one machine A lockformer forms and closes in one pass | One handling, one operator Simplest arrangement | Lowest capital and least floor space No transfer between stations | The pass rate is shared between forming and closing Closing is often the slower half, which caps throughput |
Separated in line Former feeds directly into the closer | Continuous flow between the two No intermediate stacking | Each machine runs at its own rate The usual reason to add an L-12 | The two machines must be matched on rate A faster former simply creates a queue at the closer |
Separated with a buffer Formed sections stacked between the stations | A bank of formed sections between former and closer Decouples the two rates | Absorbs the rate mismatch Each station can be run at its best pace | Needs floor space and a handling routine Stacked sections can be damaged if handled badly |
Two closers on one former Forming is faster than closing | The former feeds two closing stations alternately Balances the line | Highest throughput of the four Uses the former at its full rate | Only worth it above a substantial daily volume Two operators, more floor space |
Closing before forming Not a valid arrangement | The seam must be formed before it can be closed Sequence is fixed | N/A Included here because it is occasionally attempted | An L-12 cannot form a seam — it only closes one See the lockformers if you need both operations |
Adding an L-12 to an Existing Line Without Creating a New Bottleneck
The failure mode of adding a closing machine is moving the bottleneck rather than removing it. Measure first, then place it.
- 1. You need to know how much of the pass is forming and how much is closing. Time them separately if you can.
- 2. If closing is the slower half, separating it is worth it. If forming is, a second closer will do nothing for you.
- 3. In-line needs matched rates; buffered needs floor space. If your rates are close, go in-line; if not, buffer.
- 4. Carrying sections is the hidden cost of separation. A roller table between the two pays for itself quickly.
- 5. The L-12 closes what it is given. An upstream forming fault will pass straight through.
- 6. Compare against the baseline you took before installation. If it has not improved, the constraint is somewhere else.
- 7. A two-station line needs flexible staffing or it will idle whenever one person is absent.
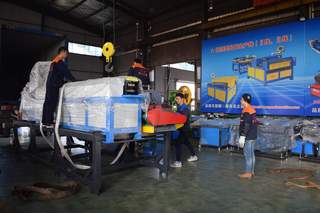
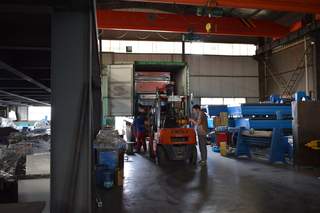
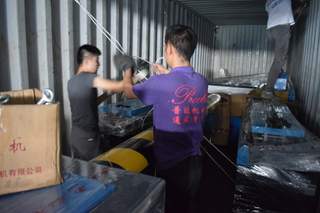
Professional Packaging & Global Shipping
Every machine is professionally packaged and secured in a container for safe delivery to your port. We send you loading photos before the ship sails.
Calculate Your Return on Investment
Based on average industry data, here is what a typical customer saves after installing this machine:
* Figures based on average customer data for a shop producing 50-200 seams/welds per day. Your actual results will vary based on production volume, labor rates, and current efficiency levels. Contact our engineers for a customized ROI calculation based on your specific operation.
Ready to Upgrade Your Pittsburgh Production?
Get a customized quote within 24 hours. Our engineers will help you configure the right machine for your specific production requirements.
WhatsApp / WeChat: +86-18355321923 | Email: jason@predamachine.com
Related Products


Buying Guides for This Machine Type
Before you request a quote: how this machine class compares, what it costs, and how to size it for your production volume.
Seam Locker Buying Guide 2026
Portable vs CNC hydraulic vs Pittsburgh L-12 closers — where each one pays for itself.
Read the guide → Buying GuidePittsburgh Lockformer Buying Guide 2026
SA-15HB vs SA-12HB vs snaplock vs S&drive: which lock profile and machine fits your duct class.
Read the guide → MaintenancePittsburgh Lockformer Maintenance Guide
Daily, weekly and annual service schedule that keeps a lockformer accurate past ten years.
Read the guide → TroubleshootingPittsburgh Lockformer Problems & Solutions
Symptom-to-cause troubleshooting table for the faults that stop a lockformer mid-shift.
Read the guide →