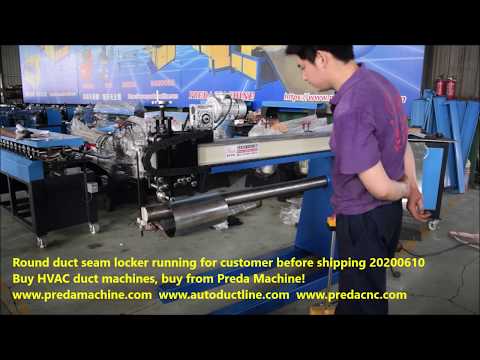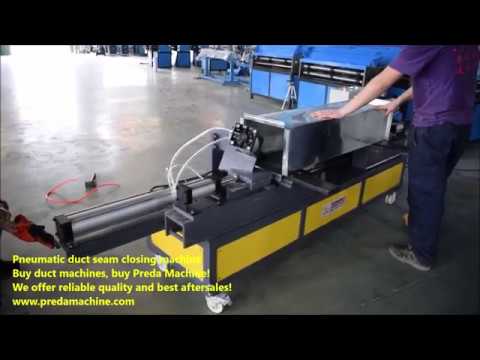


Duct Seam Closing Machine
Last updated: October 12, 2026
Pittsburgh seam closing machine for airtight, professional seam finishing on rectangular duct.
Technical Specifications
What is a Duct Seam Closing Machine?
A Pittsburgh lockformer (also called a Pittsburgh lock machine or pittsburgh machine) is a sheet metal forming machine that creates the Pittsburgh lock seam — the most widely used connection method for rectangular HVAC ductwork. The machine rolls a female pocket on one edge of the sheet and a male flange on the mating edge, allowing ducts to be assembled by simply inserting and hammering the seam closed. Pittsburgh lockformers are essential equipment in any sheet metal duct fabrication shop.
Key Features
- Consistent seam closure
- Airtight finish
- Adjustable pressure
- Stand-mounted with guide
Still Losing Money to Leaky Seams and Slow Assembly?
Every HVAC duct shop faces the same bottleneck: hammering seams closed by hand. When your team spends hours on inconsistent weld quality, your production capacity drops, labor costs rise, and deadlines slip. The Duct Seam Closing Machine is engineered to eliminate these inefficiencies — automating duct seam closing machine while delivering consistent, factory-grade quality.
In this guide, we break down exactly how this machine transforms your pittsburgh seam locker workflow, what specifications matter for your operation, and how to calculate your return on investment. Whether you run a 3-person job shop or a 50-employee production facility, understanding these details directly impacts your bottom line.
How It Transforms Your Production Line
The Duct Seam Closing Machine operates on a proven principle: duct seam closing machine should be a continuous, automated process — not a series of manual interventions. Here is the step-by-step workflow that makes this possible:
Seam Alignment
The Pittsburgh lock is hooked together and positioned in the seam closing machine, or the weld joint is aligned for welding.
Automatic Closing/Welding
Powered rollers close the seam along the full length, or welding electrodes create a continuous or spot weld — no manual hammering required.
Quality Check
The closed seam or weld is inspected for completeness and airtightness — consistent quality every time.
Discharge
The finished duct section is ready for flange installation and shipping.
Technical Specifications & Performance Data
Every specification on this machine is chosen for a reason. The table below shows not just the numbers, but what each one means for your daily production:
| Parameter | This Machine | What It Means for You |
|---|---|---|
| Control System | PLC with touchscreen | Easy programming, consistent results, minimal training |
| Construction | Heavy-duty steel frame | Vibration-free operation, 10+ year service life |
| Certification | CE certified | Meets European safety and quality standards |
| Warranty | 2 years | Peace of mind with comprehensive factory warranty |
Problems Solved: Before vs. After
We asked 50+ HVAC fabricators about their biggest production headaches. Here is how this machine directly addresses each one:
| Without This Machine | With This Machine |
|---|---|
|
✕ Hand hammering is slow and noisy
5-10 minutes per seam, worker fatigue, noise pollution |
✓ Powered seam closing in 10-30 seconds
10-20x faster, quiet operation, less fatigue |
|
✕ Inconsistent seam closure
Some seams leak, failed pressure tests |
✓ Uniform roller pressure along full length
Every seam identical, guaranteed airtight |
|
✕ Spot welding burns through thin metal
Holes in duct, rework and scrap |
✓ Precise current and time control
Perfect welds every time, no burn-through |
|
✕ Welding requires skilled labor
Hard to find qualified welders, high wages |
✓ Simple operation, minimal training needed
Any operator can produce quality welds |
Where It Fits in Your Factory
This machine is versatile enough to serve multiple production scenarios. Here are the most common configurations our customers use:
Pittsburgh Seam Closing
Closing the longitudinal seam on rectangular ducts after lock forming — the most common application in HVAC fabrication.
Spot Welding
Fast, clean spot welds for round duct assembly, flange attachment, and bracket installation — no filler material needed.
Seam Welding
Continuous or stitch welding for high-pressure ducts, stainless steel ducts, and applications requiring maximum airtightness.
Flange Fastening
Power fastening of TDC flange clips and connectors — faster and more consistent than manual screwdriving.
Frequently Asked Questions
Click each question to see the answer. These are the questions our sales engineers hear most often:
Seam Closing Machines: Mechanical Options Compared
Once forming and closing are separated, the closing machine becomes its own purchase decision. This one is the mechanical option: lower capital than hydraulic, well matched to standard gauge, and entirely adequate for most commercial work.
| Machine | Drive | Gauge | Best fit |
|---|---|---|---|
Duct Seam Closing Machine This machine — mechanical closing | Mechanical Lower capital, simpler service | Standard commercial gauge 24–22 ga comfortably | Standard gauge at moderate to high volume Also where hydraulic service is not available |
Hydraulic closing | Hydraulic Consistent pressure, heavier gauge | Heavier gauge Hydraulic force | Heavier gauge, or recurring seam leakage problems Higher capital and more service requirement |
Mechanical closing | Mechanical Comparable | Standard gauge Comparable | You want to compare mechanical options side by side Decide on throughput and service support |
Forms and closes in one pass | Mechanical One handling | Up to 1.0 mm Combined operation | You would rather not separate the two operations Simpler layout, fewer machines |
Cuts the blank | N/A Upstream | N/A Blank preparation | You are reviewing the whole rectangular line Blank accuracy affects every downstream operation |
Getting a Leak-Free Seam From a Mechanical Closer
Mechanical closing depends on set-up and edge condition. Both are controllable, and both are where nearly every seam fault originates.
- 1. The closer finishes the seam; it does not create it. An upstream forming fault will survive the closer intact.
- 2. One setting per gauge on a card at the machine. This single habit prevents most seam faults.
- 3. A burred or out-of-square edge produces an incomplete lock regardless of how well the closer is set.
- 4. Ten seconds per change. The alternative is discovering the fault on site.
- 5. The only reliable check. Do it in the first month at every batch, then periodically.
- 6. An unsupported section twists and produces a seam that varies along its length.
- 7. Zinc build-up changes the closing geometry slowly, so quality drifts rather than failing suddenly.
- 8. Two numbers that show whether the closer or the former is the real constraint.
Seam Closing Faults: Symptom, Cause, Fix
Work backwards from the seam: edge condition, then forming, then closing. Nine faults in ten are in the first two.
| Symptom | Most likely cause | What to do |
|---|---|---|
Seam leaks Closing pressure insufficient for the gauge | Looks closed from outside and is not fully closed inside The fault that reaches site | Increase closing pressure for the gauge and air-test a section Record the setting once it passes |
Seam incomplete at one end Section twisting or unsupported | The section twists as it passes A handling fault rather than a setting fault | Support the section at both ends and re-check Confirm the strip edge is square too |
Lock will not start Strip edge burred or out of square | Edge condition prevents engagement Usually traced to a worn shear blade | Deburr and square the edge and check the shear blade condition Do not force the section |
Quality drifts over weeks Zinc build-up in the closing head | Slow build-up changes the closing geometry Drift rather than sudden failure | Clean the closing head weekly with a brass brush, never steel Inspect under a bright light |
Marking along the seam Head damage or debris | A damaged head marks every metre after it Often starts after a blade change | Clean and inspect the closing head Never use steel on the working surfaces |
Machine strains at heavy gauge At the top of the specified range | A mechanical closer has a defined gauge range A specification boundary rather than a fault | Verify thickness with a micrometer and compare with the specification Consider a hydraulic closer for sustained heavy work |
Professional Packaging & Global Shipping
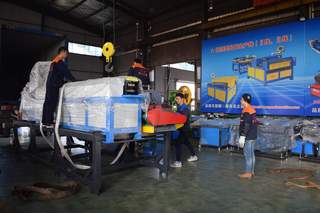
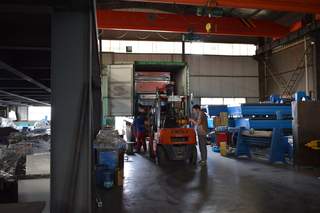
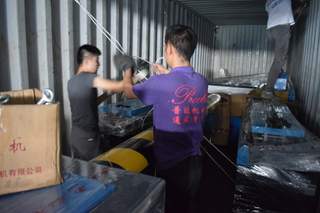
Every machine is professionally packaged and secured in a container for safe delivery to your port. We send you loading photos before the ship sails.
Calculate Your Return on Investment
Based on average industry data, here is what a typical customer saves after installing this machine:
* Figures based on average customer data for a shop producing 50-200 seams/welds per day. Your actual results will vary based on production volume, labor rates, and current efficiency levels. Contact our engineers for a customized ROI calculation based on your specific operation.
Ready to Upgrade Your Duct Production?
Get a customized quote within 24 hours. Our engineers will help you configure the right machine for your specific production requirements.
WhatsApp / WeChat: +86-18355321923 | Email: jason@predamachine.com
Related Products


Buying Guides for This Machine Type
Before you request a quote: how this machine class compares, what it costs, and how to size it for your production volume.
Seam Locker Buying Guide 2026
Portable vs CNC hydraulic vs Pittsburgh L-12 closers — where each one pays for itself.
Read the guide → Buying GuidePittsburgh Lockformer Buying Guide 2026
SA-15HB vs SA-12HB vs snaplock vs S&drive: which lock profile and machine fits your duct class.
Read the guide → MaintenancePittsburgh Lockformer Maintenance Guide
Daily, weekly and annual service schedule that keeps a lockformer accurate past ten years.
Read the guide → TroubleshootingPittsburgh Lockformer Problems & Solutions
Symptom-to-cause troubleshooting table for the faults that stop a lockformer mid-shift.
Read the guide →